
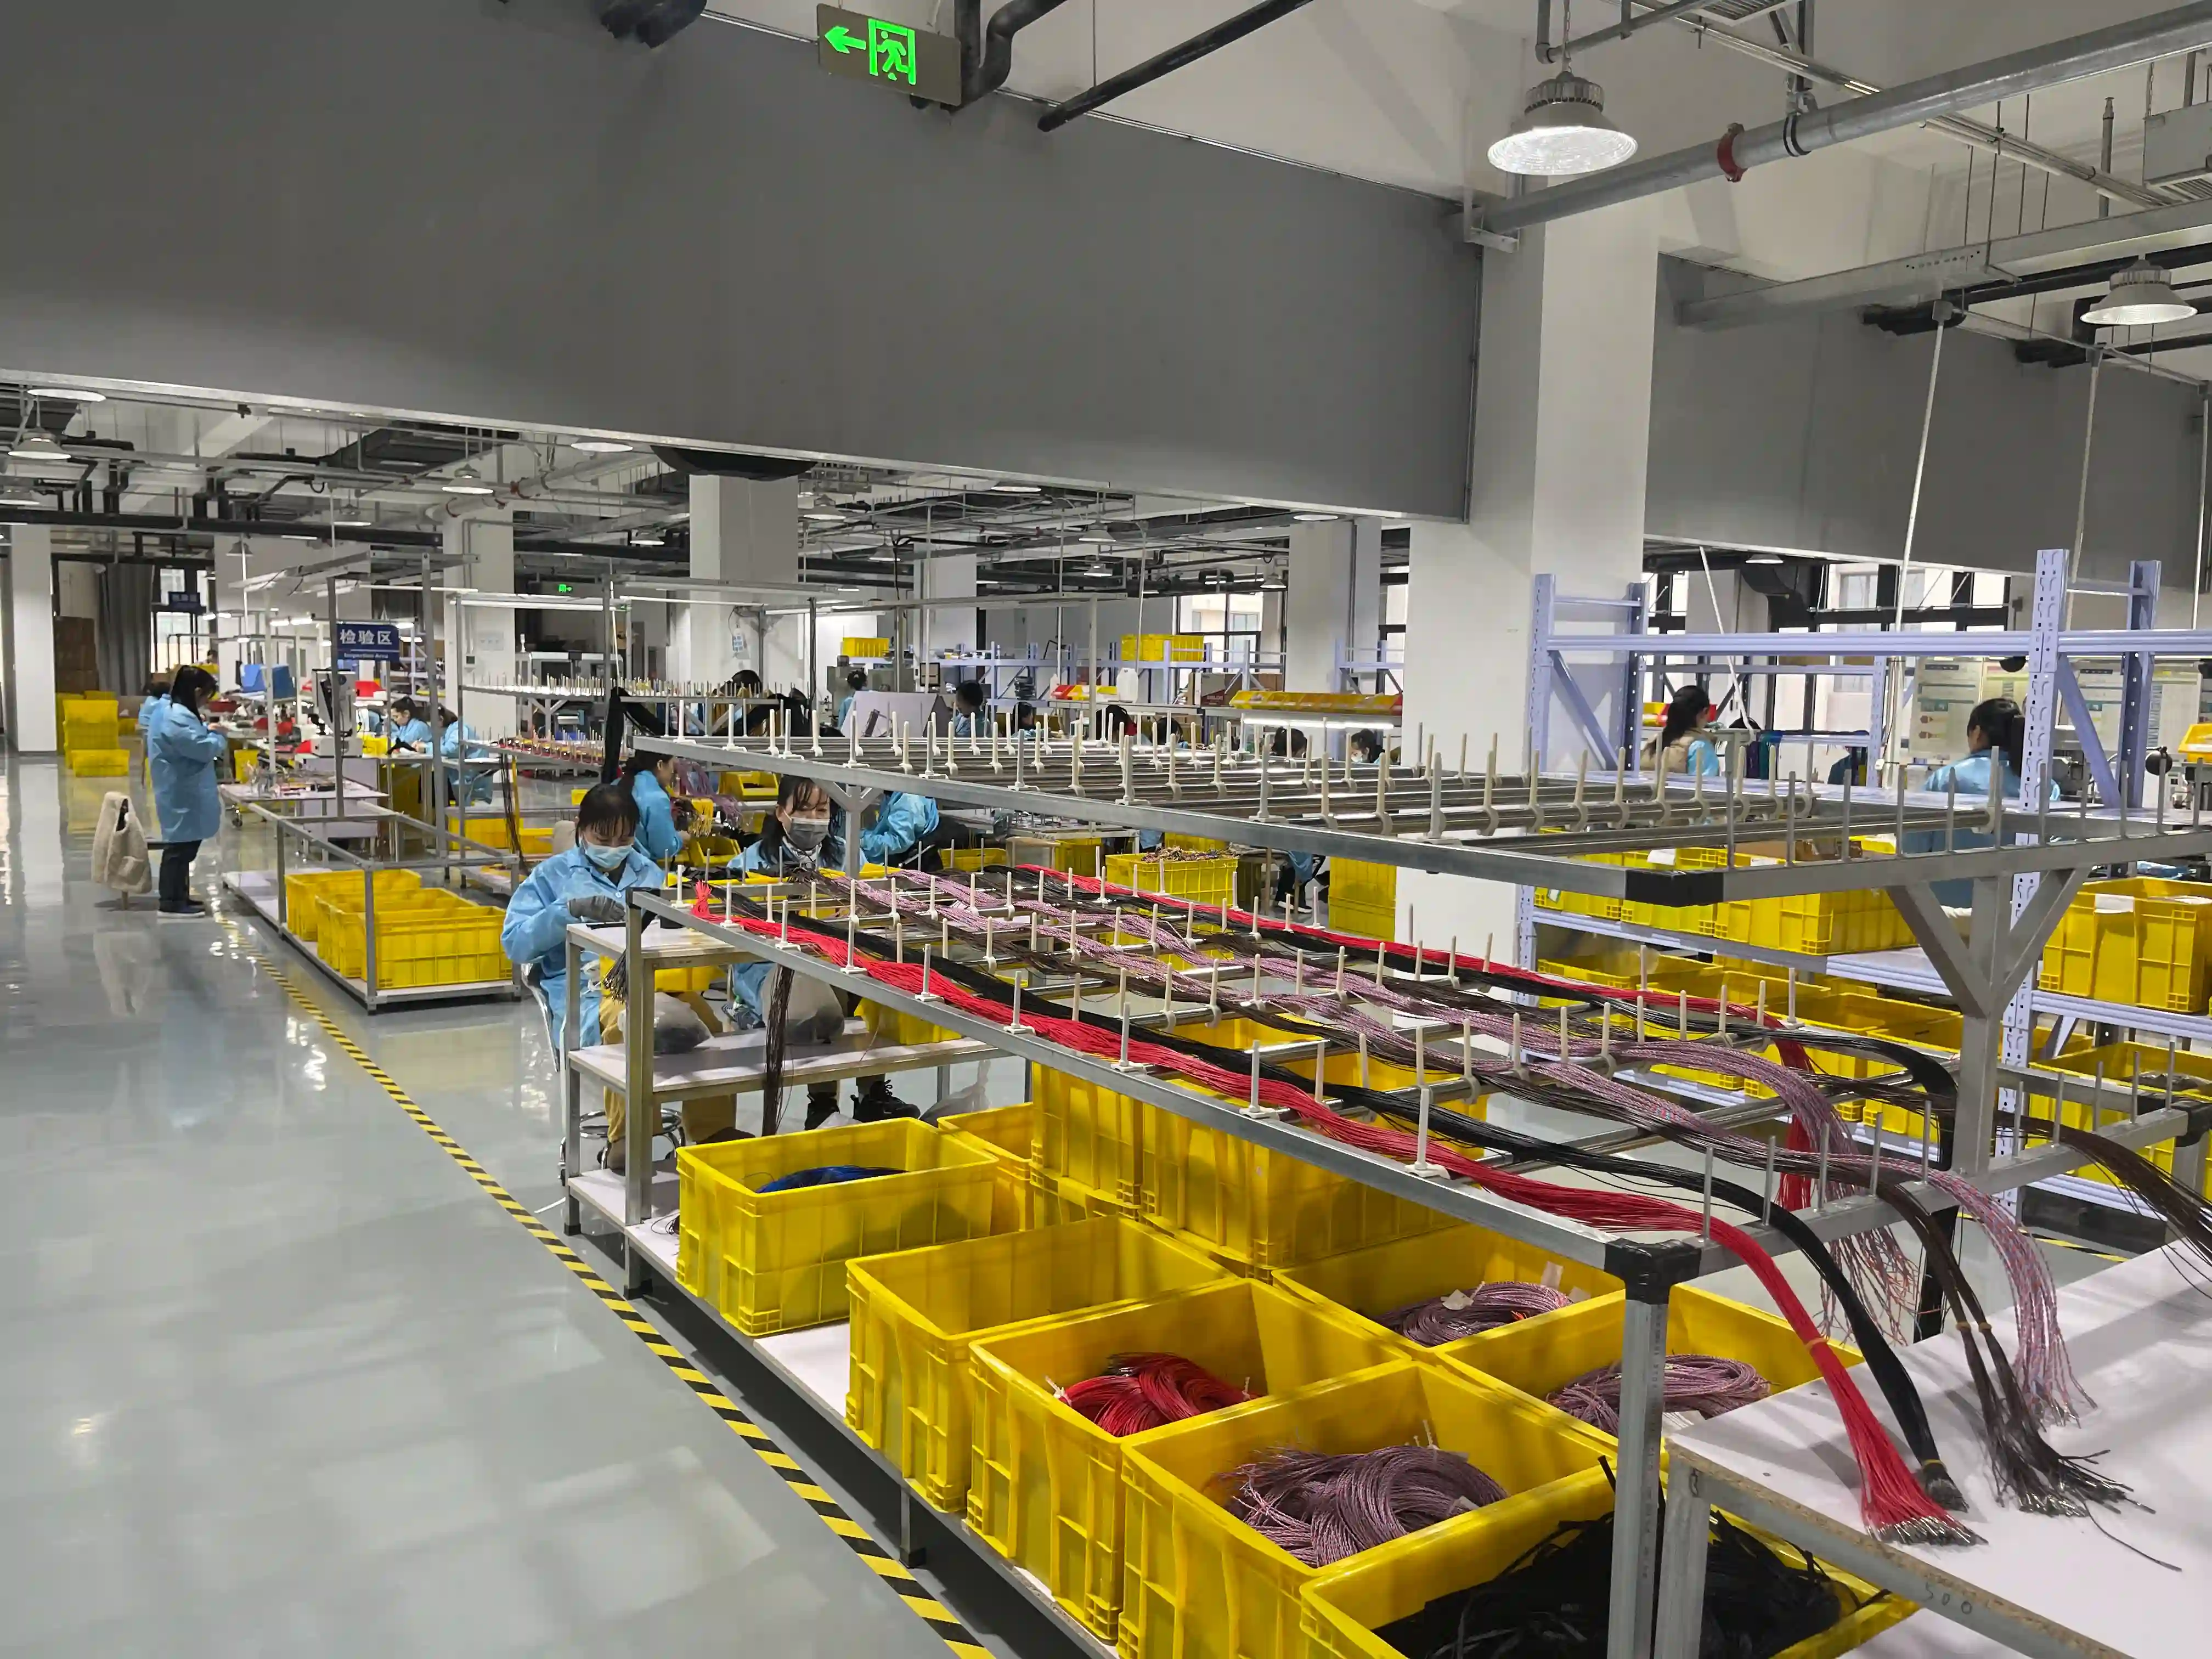
Why Your Bundling Method Choice Can Make or Break a Harness
A mining company in Western Australia lost three days of production when nylon cable ties on an excavator's main wiring harness turned brittle in 52°C ambient heat and snapped during vibration. The loose wires chafed against a hydraulic line, shorting the engine management system. A competitor running the same equipment 200 metres away had no issues — their harness supplier used stainless steel ties with silicone edge coatings.
The bundling method you select determines how well a wire harness survives temperature cycling, vibration, chemical exposure, and routine maintenance over its service life. A nylon cable tie and a stainless steel tie both hold wires together — but they fail in fundamentally different ways under stress.
This guide compares five bundling methods head-to-head: nylon cable ties, stainless steel cable ties, lacing cord, spiral wrap, and edge clips. Each section covers where the method excels, where it fails, and what IPC/WHMA-A-620 requires for acceptance.
Bundling methods compared
Max temp (SS 316 ties)
Speed difference: ties vs lacing
IPC-620 class levels
Nylon Cable Ties: The Production Workhorse
Nylon 6.6 cable ties account for over 80% of all wire harness bundling in commercial and industrial applications. A single tie installs in 3-5 seconds with a pneumatic tool such as the Panduit GTS or HellermannTyton MK9, making them the fastest bundling method for high-volume production lines.
Where Nylon Ties Excel
Where Nylon Ties Fail
UV-Stabilised vs Standard Nylon
Standard nylon ties in outdoor Australian environments (UV index 11+) can fail within 6 months. Always specify UV-stabilised (black carbon-filled) nylon for any harness exposed to sunlight. HellermannTyton T-series and Panduit PLT-M meet outdoor UV resistance requirements per UL 746C.
For indoor industrial harnesses operating between -20°C and 80°C, standard nylon cable ties remain the most cost-effective choice. Pair them with a heat shrink sleeve at connector terminations where point-load stress concentrates.
Stainless Steel Cable Ties: Extreme Environment Solution
Stainless steel cable ties handle conditions that destroy every polymer-based bundling method. Grade 304 stainless withstands continuous temperatures to 480°C; grade 316 resists salt spray and marine atmospheres where nylon corrodes within weeks. Australian mining operations in the Pilbara and Queensland coal fields specify stainless steel ties as standard for engine bay and undercarriage harnesses exposed to 50°C+ ambient heat, dust, and diesel.
| Property | SS 304 | SS 316 |
|---|---|---|
| Max continuous temp | 480°C | 538°C |
| Salt spray resistance | Moderate (500 hrs) | Excellent (2000+ hrs) |
| Tensile strength (8 mm width) | 450 N | 400 N |
| Best for | Indoor high-temp, exhaust routing | Marine, chemical plants, coastal |
Edge Coating Matters
Bare stainless steel ties can cut into wire insulation under vibration. Specify polyester or silicone-coated stainless ties for any harness in a vibration environment. The coating adds material and processing work but helps prevent insulation damage that leads to shorts.
Lacing Cord & Lacing Tape for Industrial Harnesses
Cable lacing distributes holding force across a flat, wide contact surface instead of concentrating it at a single narrow tie point. Select cord material and knotting methods to suit the operating temperature, fluids, and maintenance requirements of the industrial equipment.
Need cable lacing for your harness? Send your drawing for review via our cable lacing service.
When Lacing Is Useful
- No FOD risk: Lacing cord has no sharp trimmed tails. Cable tie tails, even when flush-cut, can fracture and become foreign object debris inside sealed equipment enclosures.
- Weight saving: Flat braided nylon tape weighs 40-60% less than an equivalent number of cable ties across a large harness — significant when multiplied across thousands of tie points.
- Distributed pressure: Lacing cord contacts the wire bundle across its full width, preventing the point-load indentation that cable ties cause on soft insulation like PTFE and FEP.
- Maintainability: Lacing is removed by cutting at one point and unwinding — no risk of cutting wire insulation with a knife, unlike cable tie removal.
Lacing Materials Compared
| Material | Temp Range | Chemical Resistance | Common Use |
|---|---|---|---|
| Waxed nylon | -55°C to 90°C | Moderate | Instrumentation, telecom |
| Waxed polyester | -55°C to 130°C | Good (acids, fuels) | Harsh industrial environments |
| PTFE (Teflon) | -200°C to 260°C | Excellent (all chemicals) | Spacecraft, high-temp zones |
| Nomex | -55°C to 220°C | Excellent (flame-resistant) | Engine bay, fire zones |
The main trade-off with lacing is speed. Hand-tied lacing takes 15-30 seconds per tie point — 5-10x slower than a cable tie. DMC's LaceLok fasteners reduce this to 5-8 seconds with material selection checked against the approved drawing. For industrial harnesses, specify lacing where pressure distribution, space, or service access justify the assembly time.
Lacing also does not provide abrasion or crush protection. Wires bundled with lacing cord alone can still shift during installation. For harnesses routed through bulkheads or along structure, pair lacing with a protective conduit or strain relief at the entry and exit points.
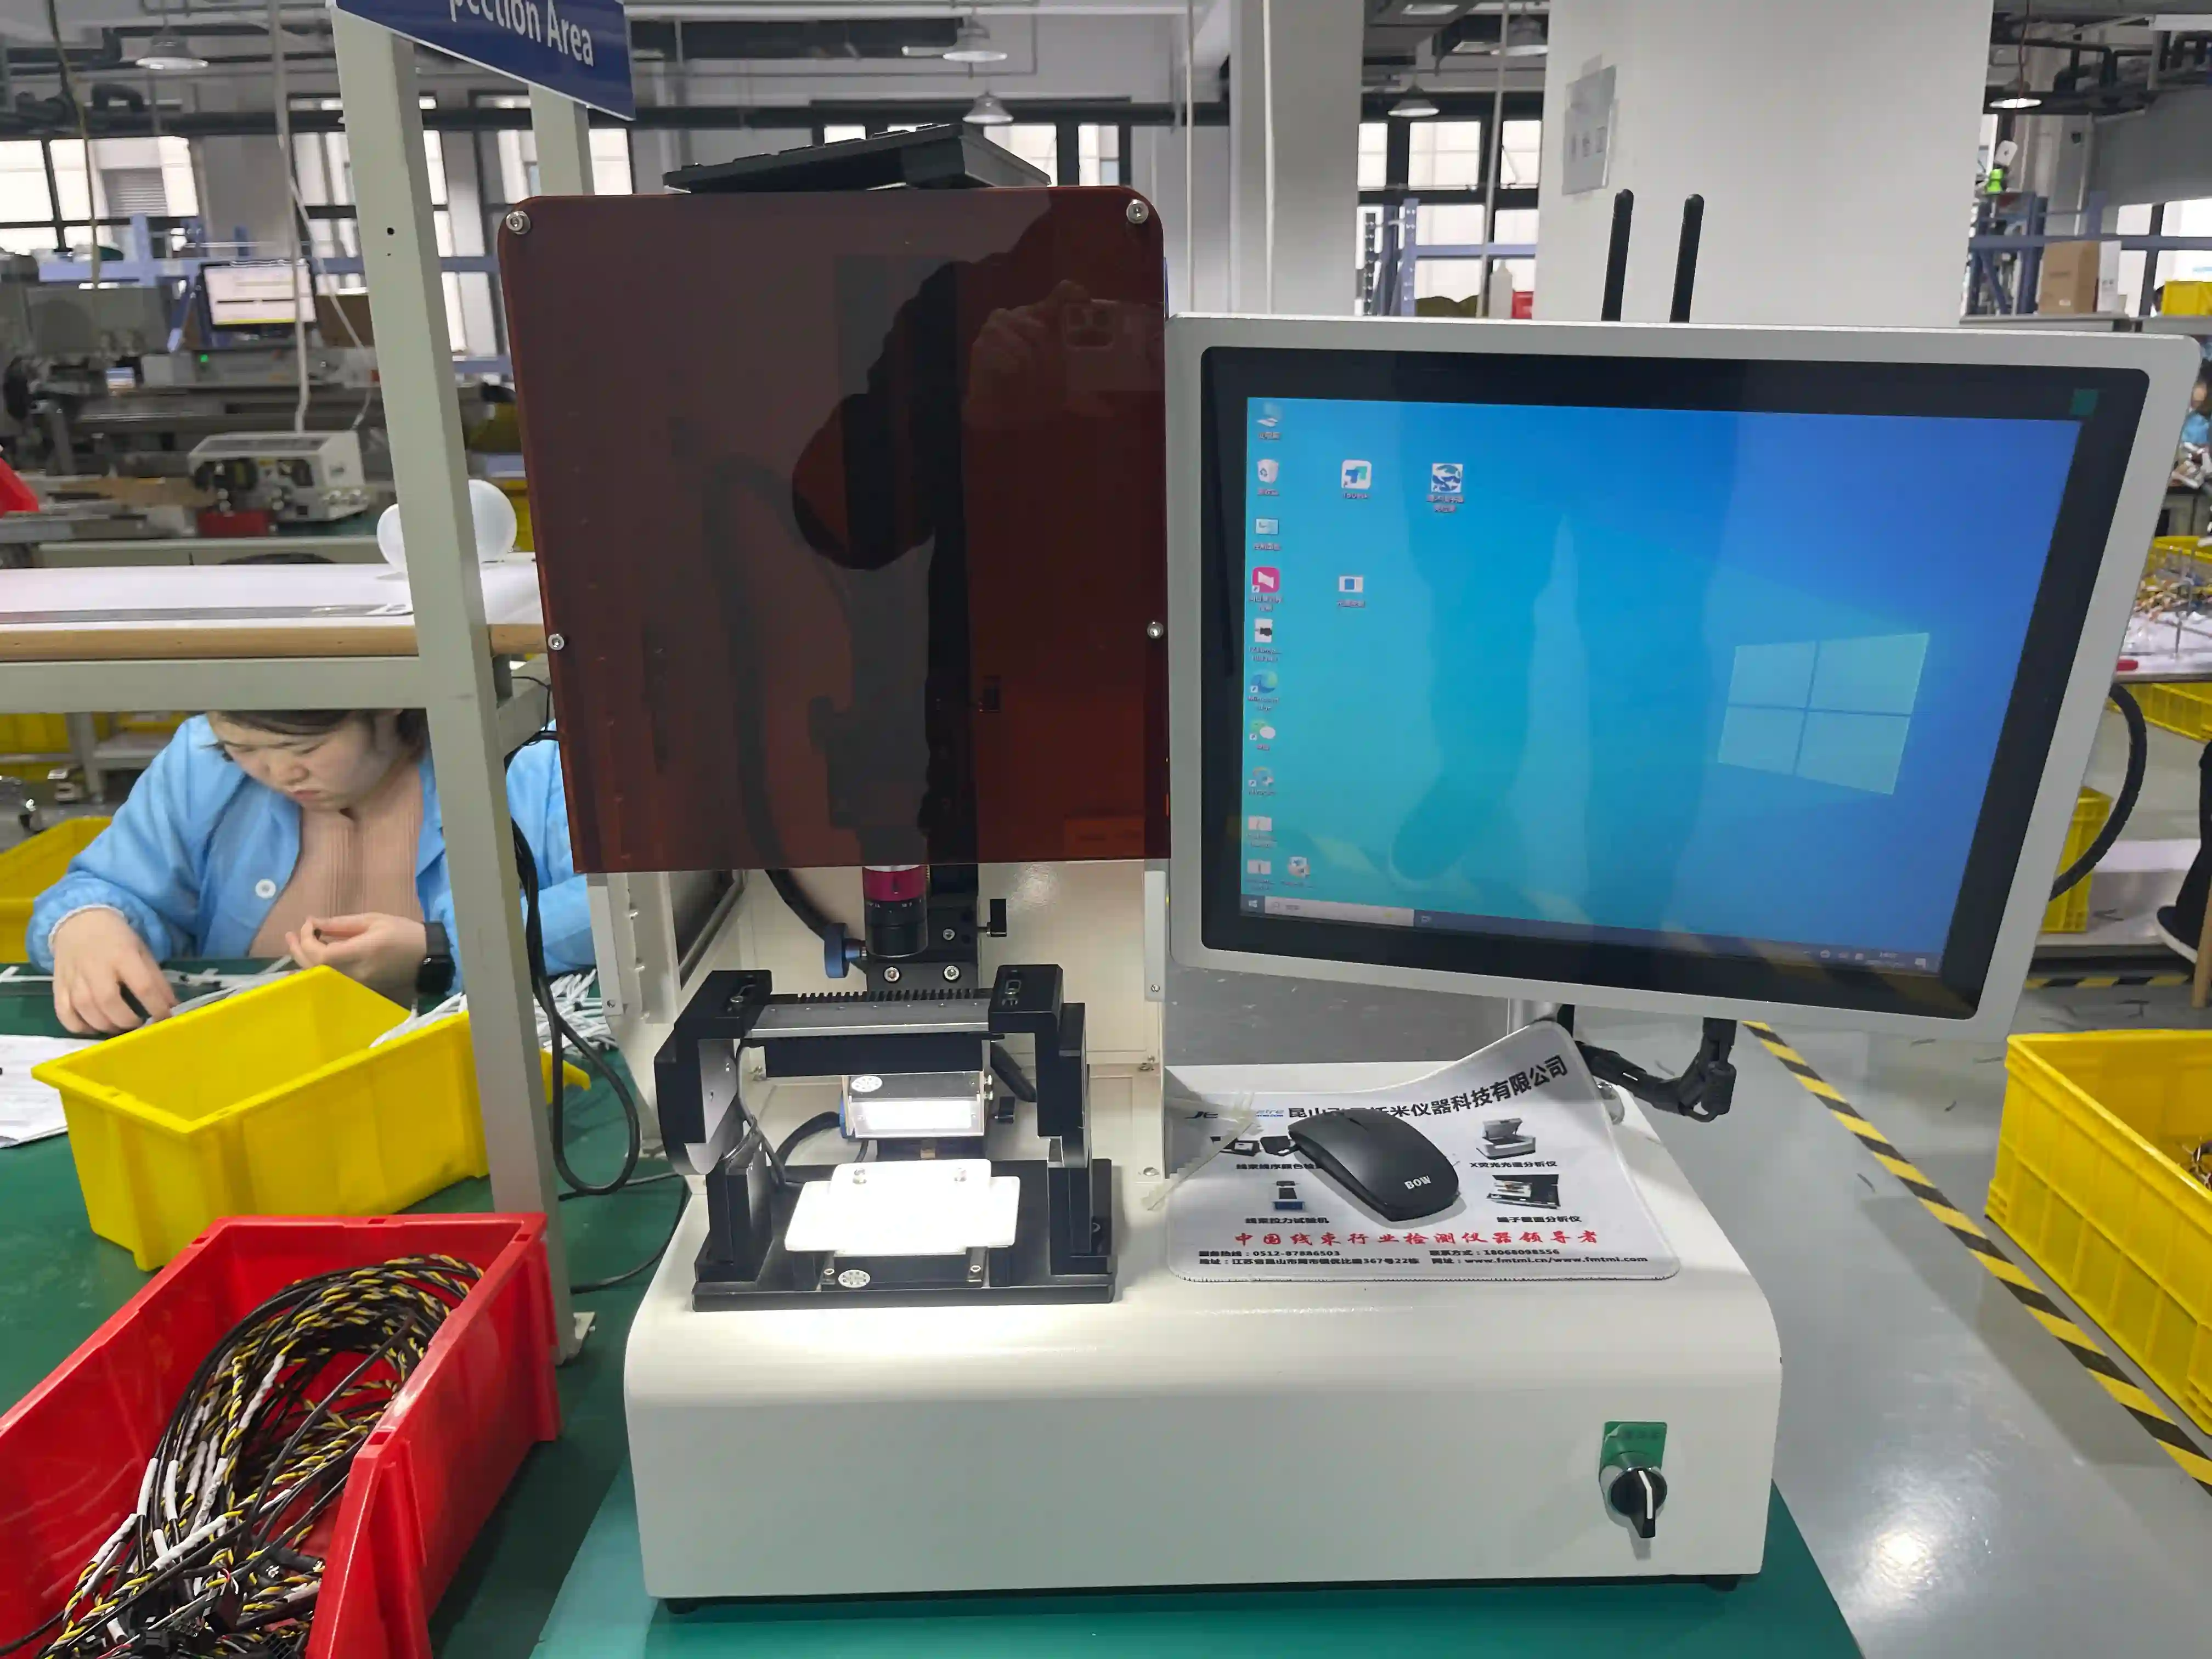
Pull-force testing equipment verifies bundling integrity meets IPC/WHMA-A-620 requirements.
Spiral Wrap & Convoluted Tubing: Bundling Plus Protection
Spiral wrap and convoluted (corrugated) tubing combine bundling with abrasion protection in a single step. Where cable ties and lacing only hold wires together, these methods also shield the bundle from mechanical damage — a requirement in harsh routing environments like vehicle underbodies, cable trays, and industrial machinery.
Spiral Wrap
- Mid-run breakouts at any point without cutting
- Easy post-installation access for maintenance
- Lighter weight than convoluted tubing
- Lower crush resistance than convoluted tubing
- Spiral gaps allow dust and moisture ingress
Diameter, material and installation work affect cost.
Convoluted Tubing
- Superior crush resistance (corrugated profile)
- Better dust and moisture sealing (split or unsplit)
- Widest range of diameters (3 mm to 100 mm+)
- Breakout points need T-fittings (pre-planned)
- Heavier and bulkier than spiral wrap
Diameter, material and breakout fittings affect cost.
In Australian automotive applications, convoluted nylon tubing (PA6 or PA12) dominates engine bay and underbody routing per most OEM specifications. The corrugated profile survives stone impacts and road debris that would tear through spiral wrap. For electronics enclosures and data centre structured cabling, spiral wrap is preferred because it allows quick access for adds, moves, and changes.
Edge Clips & Adhesive Mounts: Routing Without Drilling
Edge clips and adhesive-backed mounts are routing fasteners, not primary bundling methods. They fix a pre-bundled harness to a chassis, panel, or enclosure without drilling holes or welding studs. Bundling still requires cable ties, lacing, or tape — the clip holds the completed bundle in position.
When to Use Each
- Edge clips: Snap onto panel edges (0.5-3 mm thickness) without tools. Ideal for sheet metal enclosures and switchboards. HellermannTyton EdgeClip series supports bundles up to 40 mm diameter.
- Adhesive mounts: Stick to flat surfaces where drilling is not permitted. Use on painted panels, composite structures, and sealed enclosures. Bond strength depends on surface preparation — clean with isopropyl alcohol, apply at temperatures above 10°C.
- Push-fit mounts: Insert into pre-drilled holes (typical 6.5 mm or 8 mm). The most secure clip-based method for vibration environments. Standard in automotive and rail transport applications.
Clip spacing rule of thumb: Secure harness bundles every 150-300 mm on horizontal runs and every 200-400 mm on vertical runs. Tighter spacing (150 mm) for vibration environments per IPC standards; wider spacing (300 mm+) acceptable for static enclosures.
Side-by-Side Comparison: All Five Bundling Methods
| Criteria | Nylon Tie | SS Tie | Lacing Cord | Spiral Wrap | Convoluted |
|---|---|---|---|---|---|
| Install speed | 3-5 sec/point | 5-8 sec/point | 15-30 sec/point | ~30 sec/m | ~20 sec/m |
| Max temp (cont.) | 85°C | 480-538°C | 90-260°C* | 120-150°C | 120-150°C |
| Abrasion protection | None | None | None | Moderate | High |
| Insulation damage risk | High (point load) | High (uncoated) | Low | Low | Low |
| Mid-run breakout | Easy | Easy | Moderate | Easy | Needs T-fitting |
| Reusability | No (single use) | No (single use) | No (cut to remove) | Yes (unwind) | Yes (split type) |
* Lacing cord temperature range depends on material: nylon 90°C, polyester 130°C, PTFE 260°C.
IPC/WHMA-A-620 Bundling & Tying Requirements
IPC/WHMA-A-620 is the industry acceptance standard for cable and wire harness assemblies. Section 4 covers bundling and tying requirements across three reliability classes. Every bundling method must meet these criteria — regardless of whether you use ties, lacing, or protective wrapping.
Cable Tie Requirements
- Tails trimmed flush — sharp edges are a defect in all three classes
- Ties must not deform, cut into, or displace wire insulation
- Ties must be tight enough to prevent slipping but loose enough to rotate slightly by hand (Class 1/2)
- Class 3 (high-reliability): ties must not rotate freely around the bundle after installation
Lacing Requirements
- Lacing tension firm enough to hold bundle shape without crushing or deforming wires
- Knots must be consistent type throughout (typically clove hitch or locking stitch)
- Lacing cord ends secured with a lock stitch — loose ends are a process indicator (Class 1/2) or defect (Class 3)
- Spacing must maintain consistent bundle diameter along the harness length
General Bundling Requirements
- Bundle diameter must remain consistent — no bulges or necking between tie points
- Wires must not cross over each other within the bundle (Class 3)
- Bundling must not obstruct connector mating, unmating, or maintenance access
- All bundling materials must be compatible with the wire insulation material and operating environment
For a deeper dive into IPC-620 acceptance criteria, crimp inspection, and solder joint requirements, see our complete IPC/WHMA-A-620 guide.
Selection by Industry: What Australian Engineers Specify
Mining & Resources
Stainless steel 316 ties for engine bay and undercarriage. Convoluted PA12 tubing for all routed sections. Nylon ties only for interior cabin wiring below 60°C.
Medical Devices
Nylon ties (often detectable blue for TGA compliance) with smooth-edge profiles. Lacing on high-reliability patient-critical assemblies. No adhesive mounts in sterilised zones.
EV & Renewable Energy
UV-stabilised nylon ties for solar string wiring. SS 304 ties for battery pack high-voltage harnesses. Convoluted tubing for EV underbody routing.
Industrial Automation
Standard nylon ties for control panel wiring. Spiral wrap for cable tray runs requiring maintenance access. Edge clips for DIN rail and panel mounting.
Marine & Offshore
SS 316 ties are mandatory for all deck and bilge wiring per marine standards. Convoluted tubing with UV-resistant jacket for exposed runs. No standard nylon in salt atmosphere zones.
Cost Analysis: Material vs Labour vs Failure
Material cost per tie point tells only part of the story. Labour cost dominates for lacing-intensive harnesses, while failure cost dominates in harsh environments where the wrong bundling method causes field returns.
| Method | Tooling Required |
|---|---|
| Nylon cable tie | Pneumatic gun |
| SS 316 cable tie | SS tensioning tool |
| Lacing cord (hand) | None (manual) |
| Lacing (LaceLok) | LaceLok applicator |
Include bundling method, materials and installation requirements in the RFQ.
Tie-point count, bundling material and installation method affect assembly work. Hand lacing adds labour, while harsh environments may require stainless ties or protective tubing. Compare these requirements with field failure and replacement risks.
Quick Decision Guide: Choose Your Bundling Method
Is the operating temperature above 85°C?
Yes → Stainless steel ties (304 for dry heat, 316 for corrosive/marine) or Nomex lacing cord
Does the approved drawing specify lacing cord?
Yes → Use the specified cord and knotting method. Obtain approval before substituting cable ties.
Does the harness need abrasion or crush protection?
Yes → Convoluted tubing (high crush) or spiral wrap (moderate crush, easy access)
Is the harness exposed to outdoor UV or salt spray?
UV only → Black UV-stabilised nylon ties. Salt spray → SS 316 ties
None of the above?
Standard nylon cable ties — the fastest and cheapest method for controlled indoor environments.
References
How a typical cable tie vs lacing cord vs spiral wrap program runs with us
This is an illustrative description of a representative project type, not a specific customer engagement. As a contract assembler we do not publish customer-identifiable data.
Frequently Asked Questions
My wire harness runs through an engine bay at 150°C — which bundling method won't fail?
Standard nylon 6.6 cable ties are rated to 85°C continuous and will become brittle and snap in an engine bay. Use stainless steel 316 cable ties with silicone-coated edges for continuous exposure up to 538°C. If the harness also passes through vibration zones near the exhaust manifold, combine stainless ties with a woven cloth tape overwrap (such as Tesa 51036 rated to 150°C) for abrasion protection between the tie and wire insulation.
When should industrial harnesses use lacing cord instead of cable ties?
Lacing cord distributes pressure across a wider contact surface and avoids sharp trimmed tails. For industrial harnesses, choose cord material and knotting methods to suit temperature, fluid exposure, vibration, and maintenance access. Use the method specified by the approved drawing.
What does IPC/WHMA-A-620 require for cable tie installation?
IPC/WHMA-A-620 specifies that cable tie tails must be trimmed flush with no sharp edges — this is a defect in all three classes. Ties must not deform or cut into wire insulation. Spacing should maintain consistent bundle diameter. For Class 3 (high-reliability) applications, ties must not rotate freely around the bundle after installation.
I need to bundle 200 harnesses per day — what is the fastest method?
Nylon cable ties with a pneumatic tensioning tool (Panduit GTS or HellermannTyton MK9) are the fastest production bundling method at 3-5 seconds per tie point. Lacing cord takes 15-30 seconds per point by hand, making it 5-10x slower. For medium volumes, use hook-and-loop straps at breakout points needing future service access, combined with cable ties on permanent straight runs.
How do I choose between spiral wrap and convoluted tubing?
Spiral wrap allows mid-run breakouts without cutting — wires exit through the spiral gap at any point. Convoluted tubing provides better crush resistance but requires pre-planned breakout points with T-fittings. Automotive applications favour convoluted tubing for its stone-impact resistance. Electronics applications favour spiral wrap for lighter weight and easier maintenance access. Cost depends on diameter, material and installation work; specify these requirements in the RFQ.
Can I mix bundling methods on the same wire harness?
Yes. Most production harnesses use two or three methods across different zones. A typical industrial harness might use cable ties on the main trunk, spiral wrap through a cable tray, and lacing cord at the connector breakout where space is tight. The key rule: maintain consistency within each zone and document which method applies where on the harness drawing. IPC/WHMA-A-620 does not prohibit mixing methods.
Related Articles
IPC/WHMA-A-620 Standard Guide
Class 1/2/3 acceptance criteria, crimp inspection, and supplier audit checklist
Cable Assembly Strain Relief Guide
Overmoulding, cable glands, boots, and clamps for connector protection
Heat Shrink Tubing & Sleeving Guide
Material selection, shrink ratios, sizing, and application recommendations
Need Wire Harnesses Bundled to Your Exact Specification?
We select the right bundling method — cable ties, lacing, spiral wrap, or a combination — based on your operating environment, industry standards, and production volume. Built to IPC/WHMA-A-620 workmanship standards.